Traditionally, the pharmaceutical industry has been one of the best at coping with the challenges posed by pandemics. It has adapted to new responsibilities stemming from the increased need for efficiency and speed in manufacturing new pharmaceuticals and bringing them to market. In particular, the crisis caused by COVID-19 has highlighted the importance of delivering rapid results, increasing efficiency, and eliminating errors in – but not limited to – the vaccine manufacturing process.
A developing market that has never experienced a crisis.
The global pharmaceutical market is valued at approximately $1.25 trillion and is projected to grow at a compound annual growth rate (CAGR) of 13.74% from 2020 to 2027. The United States has the world’s largest pharmaceutical market, generating around $484.8 billion. However, other countries such as Japan and China are also experiencing rapid growth, projected to reach nearly $574 billion by 2022. Pharmaceutical supply chains have demonstrated resilience to the shock of COVID-19. Therefore, the subsequent economic crisis is not expected to significantly impact the industry in the short or long term. Pharma’s response to the pandemic – related to vaccine development and distribution – has made headlines. However, many of the challenges facing the industry are not solely related to the coronavirus.
Pharmaceuticals 4.0 – the digital transformation
The impact of digital transformation in the pharmaceutical industry is broad and deep. Many results are already being achieved, and many opportunities will open up in the near future, also due to the pandemic. Pharmaceutical companies leading the future of the industry are highly vigilant and discerning. Trends are beginning to take shape on the horizon. This is because the pharmaceutical industry presents specific sensitive issues related to safety, regulations, and efficiency in manufacturing and distribution. The development of AI systems, closely linked to predictive software, is at the top of the list. Another major theme is big data analytics capabilities. Implementing and managing digital processes effectively can be a challenge, but failing to adopt digitalization could pose even greater risks.
Efficient development to improve time to market.
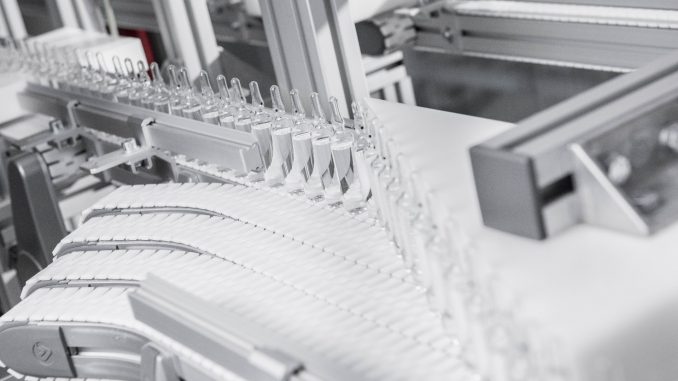
The number of clinical trials has increased significantly over the years. From 2000 to February 2021, 366,000 clinical research cases were completed worldwide. This number has increased at the same rate as investments in research and development. Investments reached $186 billion in 2019, the last year for which data is available. Pharmaceutical companies strongly support research, but one of the most important areas relates to production efficiency. It is essential to start with an efficient production line design to accelerate time to market. This leads to the need for customization with turnkey solutions that can ensure efficiency and flow continuity, along with a continuous control system. Flow balancing with buffer solutions is a critical aspect. Furthermore, preventing unnecessary errors or mistakes is of high importance, for example, due to labeling, etc. The process can be easily improved with a few simple changes, which can be easily integrated into the production line design.

Production control and monitoring
Production control and monitoring are fundamental to ensuring that pharmaceuticals are adequate, safe, and reliable. Therefore, the standard is continuous monitoring of the production process through objective measurements at all stages of production. This allows pharmaceutical companies to obtain crucial real-time data on the quality and performance of the machinery, materials, and drugs themselves. The overall goal is to ensure the highest possible quality of products brought to market. For this reason, it is important that control and monitoring processes are continuous and phased. Furthermore, automated systems achieve a level of consistency, cost savings, and safety that manual operations cannot. Predictive and simulation software can contribute even more significantly to finding suitable solutions to minimize hidden costs. Another benefit is the early detection of defects, before high-investment expenditures are made.
The future of the pharmaceutical market: simple solutions to complex problems.
Due to its unique procurement practices, the pharmaceutical industry has developed technologies now being applied in other industries. One example is serialization. Pharmaceutical serialization is the process of assigning a unique code to the packaging of each drug and printing that code on the packaging in some way. There are two main points in this definition. First is the unique code and second is the packaging of the drug. This technology can also be useful for other industries, such as food production. Even more benefits can be achieved there, including for consumers.
New challenges emerged through COVID-19.
In the future, its processes will become even more technology-oriented. On the other hand, the experience of COVID-19 has taught us that it is necessary to simplify access to treatment and medication for a large segment of the population. The drugs themselves need to become more patient-friendly, with patients clearly understanding the dosage, administration, and effects. Serialization is key to meeting this requirement. Furthermore, the supply chain will have to implement processes leading to increasingly ‘smarter’ drugs and improve the efficiency of product development, packaging, and market entry. Therefore, enhancing production capacity plays a vital role in this process, as it is crucial in enabling rapid access to treatment with necessary medications.